
Stock Sanat Specialized Magazine

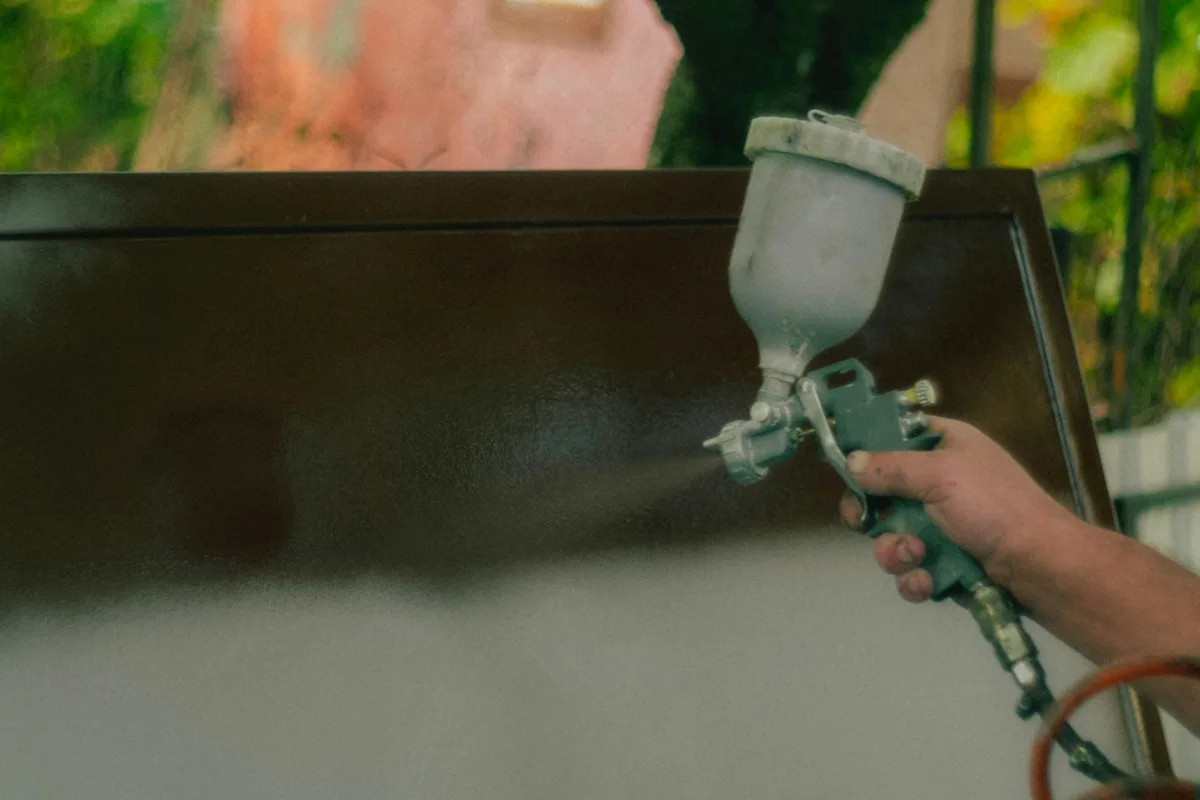
The paint is on the hull, the spray gun is still running, and nobody knows yet if the film is thick enough. Waiting for the dry film gauge is too late. By then the coat has cured and fixing it costs a full extra coat.
This guide explains how to control wet film thickness marine paint readings while the coating is still wet. It covers the comb gauge, the WFT to DFT calculation, the effect of thinner and the common mistakes. It is written for painting foremen, coating inspectors and technical managers working onboard or in dry dock.
Table of Contents
Wet Film Thickness Marine Paint Basics: What WFT Tells You
Wet film thickness (WFT) is the thickness of the coat measured right after application, while the solvent is still in the film. Dry film thickness (DFT) is what remains after the coat has cured.
The project specification sets a DFT for every coat. The painter cannot measure DFT on a wet coat, so the wet film thickness marine paint reading is used as a live estimate. It tells the applicator to add more paint or to slow down before the coat dries.
- WFT: measured seconds after spraying, with a comb gauge.
- DFT: measured after curing, with an electronic gauge.
- Volume solids: the share of the paint that stays on the surface after the solvent leaves.
The link between the three is simple. A coat with 60% volume solids loses about 40% of its wet thickness as solvent evaporates. The wet film thickness marine paint check turns that fact into a daily working number.
Why Check Wet Film Thickness Marine Paint Onboard Before the Coat Dries
A thin coat is a hidden defect. It looks fine today and fails early. A coat that is too thick can crack, trap solvent or cure too slowly. Both errors are cheaper to fix while the paint is wet.
- A low reading lets the crew add a second pass at once, in the same coat window.
- A high reading lets the crew stop before sags, runs and solvent entrapment appear.
- A recorded reading gives the inspector evidence for each coat of the system.
- It protects the owner, because a failed system often traces back to uncontrolled film build.
Paint makers state minimum and maximum DFT in the data sheet. The wet film thickness marine paint check is how the crew stays inside that range from the first pass. For the bigger picture of a docking job, see our dry-dock coatings checklist and the marine coating system guide.
WFT to DFT Calculation for Wet Film Thickness Marine Paint
The WFT to DFT calculation for wet film thickness marine paint uses the volume solids figure from the paint data sheet.
WFT = DFT ÷ (volume solids ÷ 100)
For example, take a coat specified at 200 µm DFT with a volume solids of 60%. The target is 200 ÷ 0.60 = 333 µm of wet film. These numbers are only an example. Always use the DFT from your specification and the volume solids from the data sheet of the actual product.
The same formula works backwards. If the gauge shows 333 µm wet and the volume solids is 60%, the expected dry film is about 200 µm. This is an estimate. The wet film thickness marine paint reading never replaces the final DFT measurement.
Thinning and Film Thickness: Effect on Wet Film Thickness Marine Paint Targets
Thinner adds volume but no solids. When you thin the paint, volume solids falls and the wet film must be thicker to reach the same DFT.
To adjust the calculation, divide the data sheet volume solids by 1 plus the thinner share. With 5% thinner by volume, the 60% solids paint of the example becomes 60 ÷ 1.05 = 57.1%.
| Example case (200 µm DFT) | Volume solids as applied | Target WFT |
|---|---|---|
| No thinner | 60% | 333 µm |
| 5% thinner by volume | 57.1% | 350 µm |
| 10% thinner by volume | 54.5% | 367 µm |
The table uses hypothetical values to show the trend. Thinning also changes spray behaviour and cure. Stay within the thinner type and maximum amount in the data sheet. Over-thinning can cause sagging, and the wet film thickness marine paint target must be recalculated each time the mix changes.
Tools: WFT Comb Gauge and Notch Gauge Standards
The usual tool for wet film thickness marine paint checks is the WFT comb gauge. It is a thin metal or plastic plate with teeth of different lengths along its edges. Each tooth is marked with a thickness value. Some versions have two scales, one in micrometres and one in mils.
ASTM D4414 describes the practice of measuring wet film thickness with notch gauges. Its scope covers rectangular notch gauges and circular types. You can read the title and scope on the ASTM D4414 standard page. ISO 2808 is the wider standard for film thickness methods on paints and varnishes, and it also covers wet film methods.
- Comb or notch gauge: cheap, fast and used for every coat.
- Wheel gauge: an eccentric wheel, used on flat, smooth surfaces.
- Clean cloth and thinner: to wipe the gauge after each reading.
Keep a spare gauge onboard. Dried paint on the teeth ruins the scale, so a bent or clogged gauge should be replaced, not cleaned with a blade.
How to Check Wet Film Thickness Marine Paint Step by Step
The method is the same for brush, roller or airless spray work. Follow these steps for each coat.
- Confirm the target WFT from the specification DFT and the volume solids, including the thinner share.
- Choose a gauge whose scale includes the target value in its middle range.
- Apply the coat and measure at once, before the solvent starts to flash off.
- Place the gauge on the wet film at a right angle, with the end teeth firmly on the steel.
- Press down lightly and pull the gauge straight off. Do not slide it across the surface.
- Read the highest tooth that is wet. The film thickness lies between that tooth and the next dry one.
- Wipe the gauge clean, then repeat at several spots.
- Log the readings, location and time, and tell the sprayer to correct any low area.
A 90 degree angle matters. A tilted gauge sits on the paint instead of the steel, and the reading is wrong. On curved areas such as the bilge turn, hold the gauge along the flat direction of the surface.
Marine coating data
Need volume solids and DFT data for your coating system?
Bajak epoxy systems come with technical data sheets that list volume solids and film thickness. Send your vessel, areas and docking date for a tailored quotation.
How Many Readings and Where to Take Them
One reading means nothing. Paint thickness varies across a plate, and every pass of the gun leaves a slightly different film.
- Take readings at different heights and widths of the area, not at one easy spot.
- Average the readings, and look at the lowest ones, not only at the average.
- Check edges, welds, corners and bolt heads, where films tend to be thin.
- Measure again after any correction pass.
The number of readings per area is set by the project specification, the paint maker or the owner. If it is not stated, agree it with the inspector before work starts. Then the wet film thickness marine paint records can be compared with the final DFT report.
Airless Spray Film Build: Controlling WFT While Spraying
Airless spray film build depends on a few settings that the sprayer controls every minute.
- Tip size and pressure: set by the paint data sheet, not by habit.
- Gun distance: keep it constant, and hold the gun square to the surface.
- Travel speed: a slower hand lays a thicker film.
- Overlap: each pass should overlap the last by about half, to avoid stripes of thin and thick film.
Check wet film thickness marine paint readings after the first few passes of a new area. Adjust speed or overlap, then check again. This habit costs a minute and saves a recoat. Remember that a stripe coat on edges and welds is separate from the full coat, so check it too. The general painting sequence is explained in how to paint a ship hull.
Common Errors That Spoil Wet Film Thickness Marine Paint Readings
- Late measurement: fast-drying paints lose solvent within minutes, so a late reading is too low.
- Rough surface: on blasted or pitted steel the gauge rests on the peaks, so readings are less reliable. Use the same method everywhere and compare like with like.
- Wrong gauge range: a scale that ends near your target gives poor accuracy.
- Dirty or damaged gauge: dried paint hides teeth and distorts the scale.
- Wrong volume solids: using the figure of another product or batch ruins the calculation.
- Ignoring thinner: the target must be recalculated after every thinning change.
The surface under the coat also matters. Poor preparation causes defects that no gauge can fix. See marine paint surface preparation for the steps before painting.
Limits of the Method: Confirm With a Dry Film Gauge
Wet film thickness marine paint readings are an estimate. Notch gauges are less precise than dry film instruments, and the result depends on the operator. The ASTM practice itself says the wet film method should not be used to verify the non-volatile content of the paint.
Use the wet reading to steer the job, and use the dry reading to accept it. After the coat has cured as stated in the data sheet, measure DFT with a calibrated electronic gauge. Our guide on marine paint cure time explains when a coat is ready for that check.
If the dry reading is below the specified minimum, add a further coat as the paint maker recommends. If it is above the maximum, ask the paint maker for advice before overcoating.
Get Marine Coatings With Clear Film Thickness Data
Stock Sanat Caspian is the exclusive Bajak representative since 2020. Tell us your vessel, the areas to coat and the specified DFT. We will suggest suitable products and send the technical data sheets with the volume solids you need for the wet film thickness marine paint calculation.
- Contact us to request a quote for marine coatings
- Browse Bajak marine epoxy paints
- Browse all marine paints
- See the Bajak polyurethane topcoat
Frequently Asked Questions
What is wet film thickness in marine paint?
Wet film thickness is the thickness of a paint coat measured right after application, while the solvent is still in the film. In wet film thickness marine paint work, it is checked with a comb gauge to estimate the dry film that will remain after curing.
How do you calculate WFT from DFT?
Divide the specified DFT by the volume solids of the paint as a fraction. For example, 200 µm DFT with 60% volume solids gives 333 µm WFT. This is only an example. Use the volume solids from the data sheet and correct it if thinner is added.
How do you use a WFT comb gauge?
Press the gauge on the wet film at a right angle, so the end teeth touch the steel. Pull it straight off and read the highest tooth that is wet. The film thickness lies between that tooth and the next dry one. Wipe the gauge after each reading.
Does thinner change the wet film thickness needed?
Yes. Thinner adds volume but no solids, so wet film thickness marine paint targets rise, because volume solids as applied falls. The wet film must then be thicker to reach the same DFT. Recalculate the target each time the thinner share changes, and stay within the limit in the paint data sheet.
How many WFT readings should be taken?
For wet film thickness marine paint checks, the number is set by the project specification, the paint maker or the owner, so agree it with the inspector before painting. As a rule, take readings at many spots, including edges and welds, and look at the lowest values as well as the average.
Is WFT enough to accept the coating?
No. WFT is an estimate used to steer the application. Notch gauges are less precise than dry film instruments. After the coat has cured, measure the dry film thickness with a calibrated gauge and compare it with the specified minimum and maximum.
Recent Posts